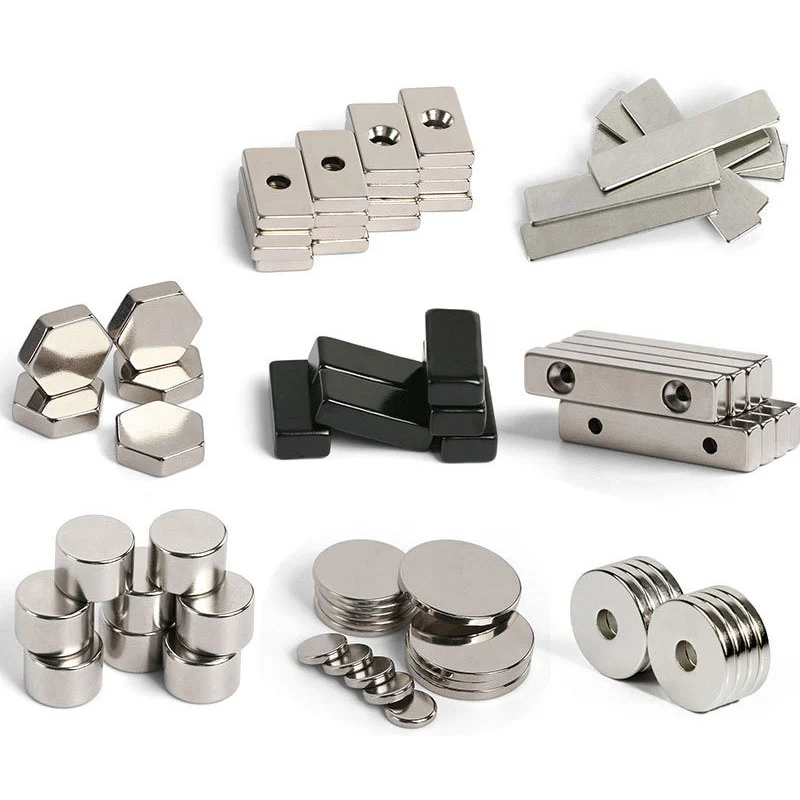
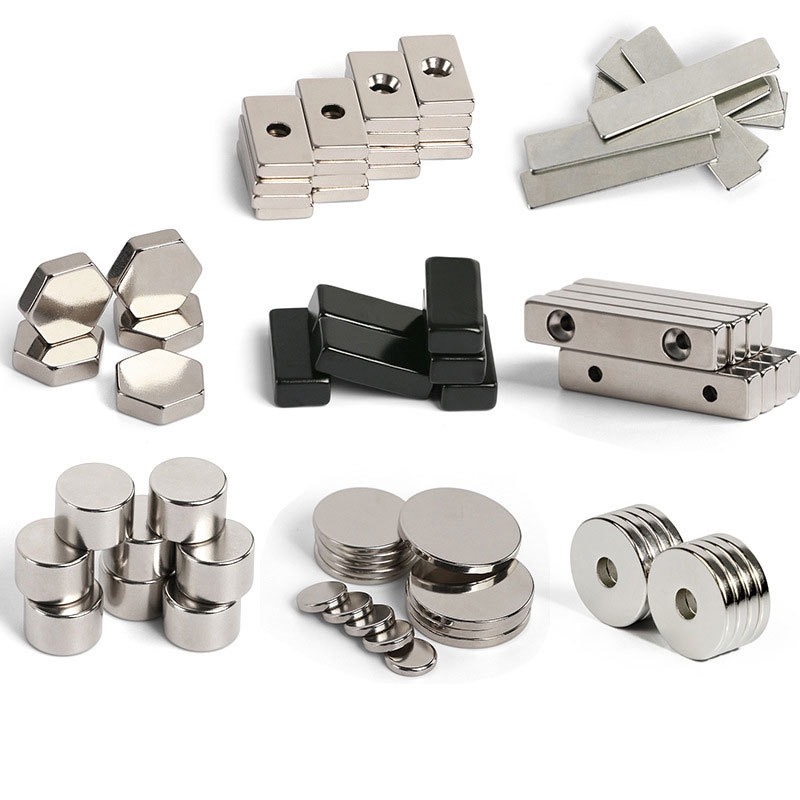
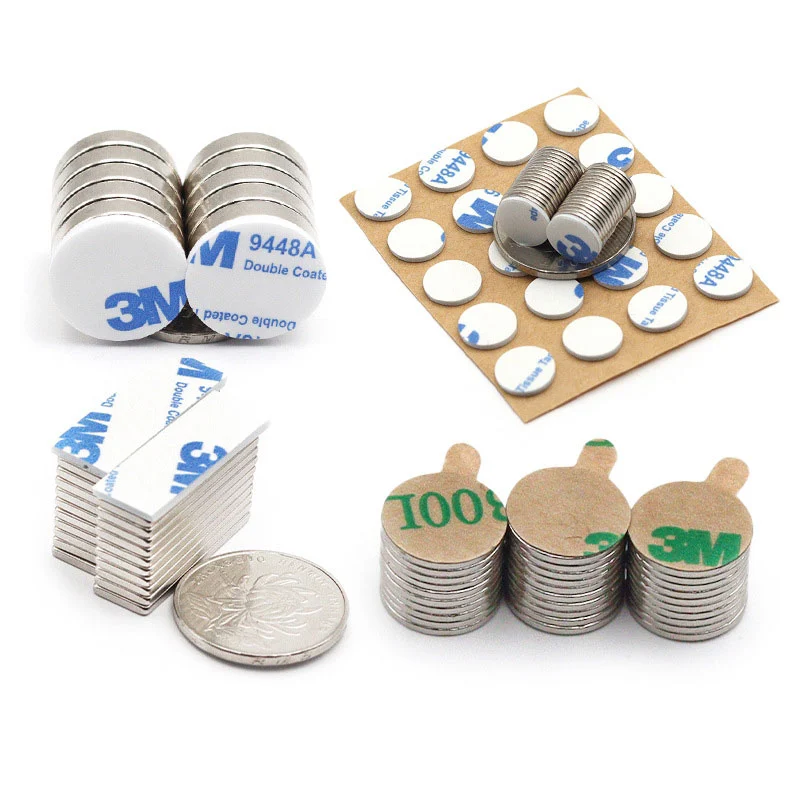
Specifically engineered to withstand the rigorous conditions of industrial environments, our industrial strength magnets provide reliable magnetic performance in applications where failure is not an option. Utilizing material formulations optimized for mechanical durability, temperature resistance, and corrosion protection, these magnets deliver consistent magnetic force in motors operating at elevated temperatures, material handling systems experiencing mechanical shock, and processing equipment exposed to chemicals or moisture. Our three decades of manufacturing expertise ensure every industrial strength magnet meets the exacting requirements of modern industrial applications.
When a magnet fails on a production line, the cost is measured in downtime, scrap and unplanned maintenance — not in the price of the component. That is why our industrial strength magnets are specified by motor manufacturers, magnetic separation integrators, automation builders and chemical processing plants that cannot afford a mid-shift failure. Every grade we supply — from high-coercivity neodymium magnets to SmCo magnets and ferrite magnets — is selected against the real operating conditions of your equipment: temperature, corrosion exposure, vibration and magnetic circuit geometry.
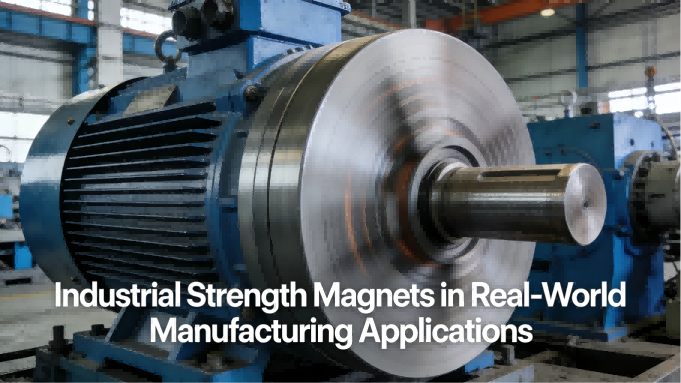
Industrial strength magnets engineered for motors, separators, automation and processing equipment
Mechanical Durability & Shock Resistance
Industrial applications often involve vibration, impact and mechanical stress that can fracture standard magnets. Our industrial strength magnets are engineered with enhanced fracture toughness through optimized microstructure control and strategic material additives. We conduct comprehensive mechanical testing including drop tests from 1.5 metres, vibration testing per MIL-STD-167 and compressive strength verification to ensure survival in demanding industrial environments.
Extended Temperature Performance Range
Industrial equipment frequently operates at elevated temperatures. Our specialized material formulations provide working temperature ranges from −50°C to +600°C depending on material type. For neodymium magnets we offer EH and AH grades with temperature coefficients as low as −0.07%/°C, while our samarium cobalt magnets maintain performance up to 350°C and Alnico magnets to 600°C — ensuring reliable operation in ovens, motors and thermal processing equipment.
Corrosion Protection for Industrial Environments
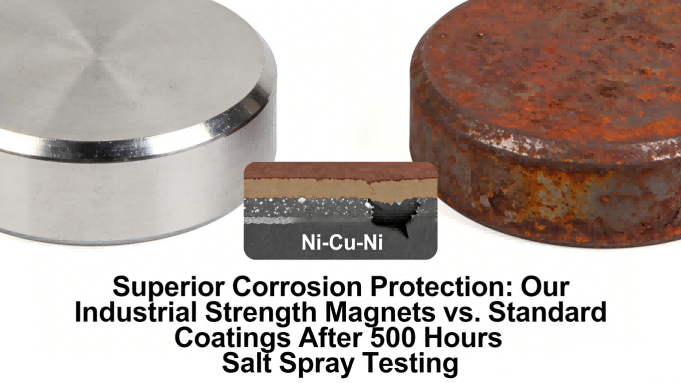
Industrial settings often expose magnets to moisture, chemicals and corrosive atmospheres. Our standard Ni-Cu-Ni triple-layer electroplating (minimum 15μm total thickness) provides 500+ hours of neutral salt spray protection per ASTM B117. For extreme conditions we offer epoxy coatings, gold plating or specialized passivation treatments that withstand aggressive industrial chemicals while maintaining dimensional stability of the industrial strength magnets.
Primary Industrial Applications
M
Motor & Generator Systems
High-torque industrial motors, servo motors, wind turbine generators and alternators requiring temperature stability and consistent magnetic performance. See our motor magnet range for rotor and stator designs.
Precision positioning systems, robotic grippers, linear actuators and sensor applications requiring reliable magnetic performance in automated environments.
P
Processing Equipment
Pumps, compressors, mixers and processing machinery operating in chemical, food processing, pharmaceutical and manufacturing facilities.
The following table compares the key performance characteristics of different magnet materials suitable for industrial applications. Selection depends on specific requirements for temperature, corrosion resistance, magnetic strength and cost. If you need a higher-energy strong magnet for a compact design, NdFeB is usually the starting point; if thermal stability dominates, SmCo or Alnico is the better answer.
NdFeB, SmCo, Alnico and ferrite industrial magnets — a side-by-side material comparison
Quality Assurance for Industrial Applications
Every batch of industrial strength magnets undergoes our 12-point quality verification protocol specifically designed for industrial applications. This includes dimensional verification with coordinate measuring machines (CMM), magnetic performance testing at both room temperature and elevated temperatures, coating thickness verification using X-ray fluorescence, salt spray testing per ASTM B117, mechanical shock testing and thermal cycling between −40°C and maximum operating temperature. Our IATF 16949 certification ensures automotive-grade quality management, while ISO 9001:2015 provides the framework for consistent manufacturing processes.
Recognising that industrial magnets often ship directly to manufacturing facilities, we employ industrial-grade packaging solutions. Each magnet is individually separated in 8-cell reinforced inner packaging with non-magnetic spacers, then packed in heavy-duty export cartons or wooden crates with corner protection. Our packaging is validated to withstand transit vibration per ISTA 3A standards and includes clear labelling with handling warnings, magnetic strength indicators and material safety data sheets when required.
Frequently Asked Questions About Industrial Strength Magnets
Which industrial magnet material is best for my application?
Start with three parameters: operating temperature, corrosion exposure and required holding or driving force. Below 120°C with a need for maximum strength, NdFeB is the most cost-effective choice. Between 150°C and 350°C, SmCo delivers stable output where NdFeB would suffer irreversible loss. Above 350°C, Alnico is the practical option. For high-volume, cost-driven holding duties, ferrite remains the workhorse. Our engineers will review your drawing and duty cycle and recommend the grade, coating and geometry before you commit to tooling.
Can you manufacture industrial strength magnets to a custom drawing?
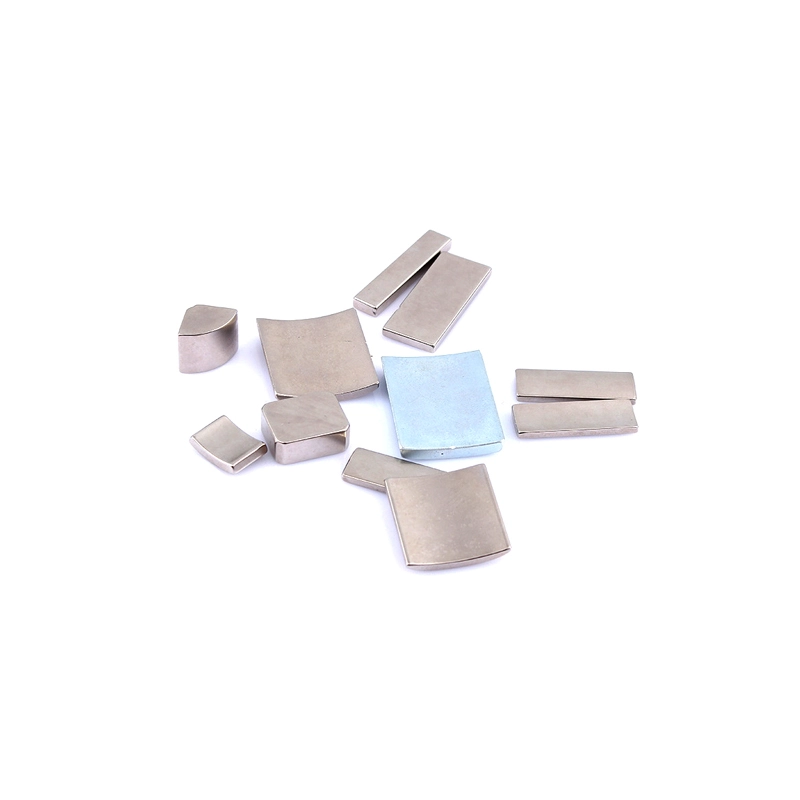
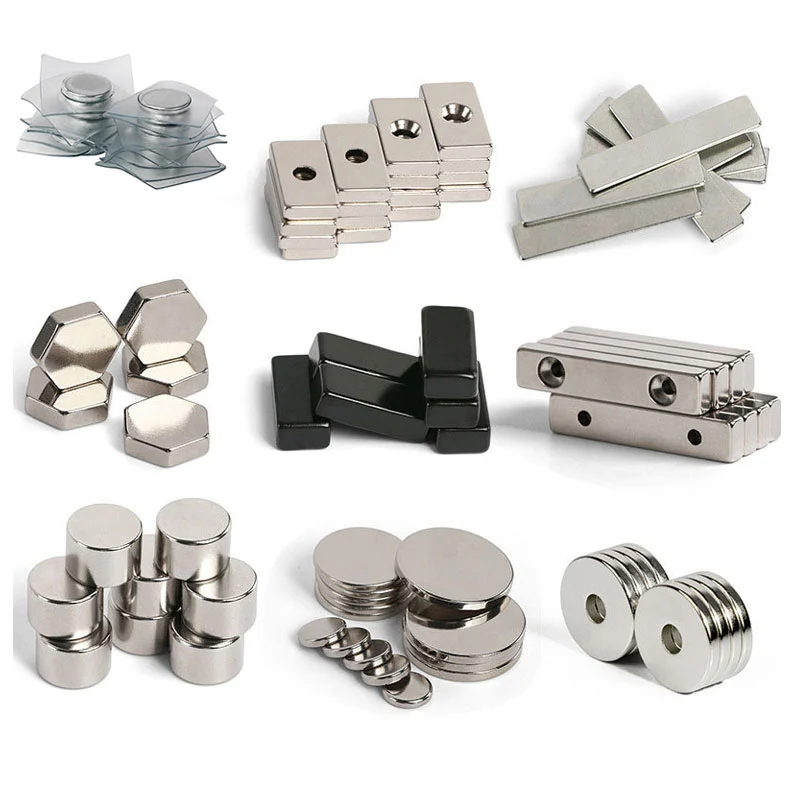
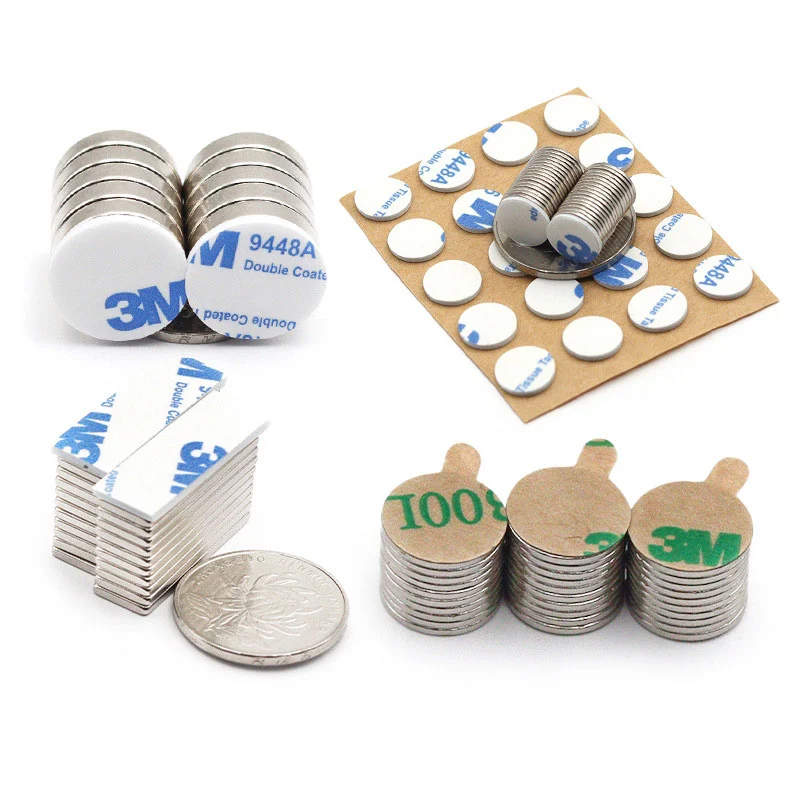
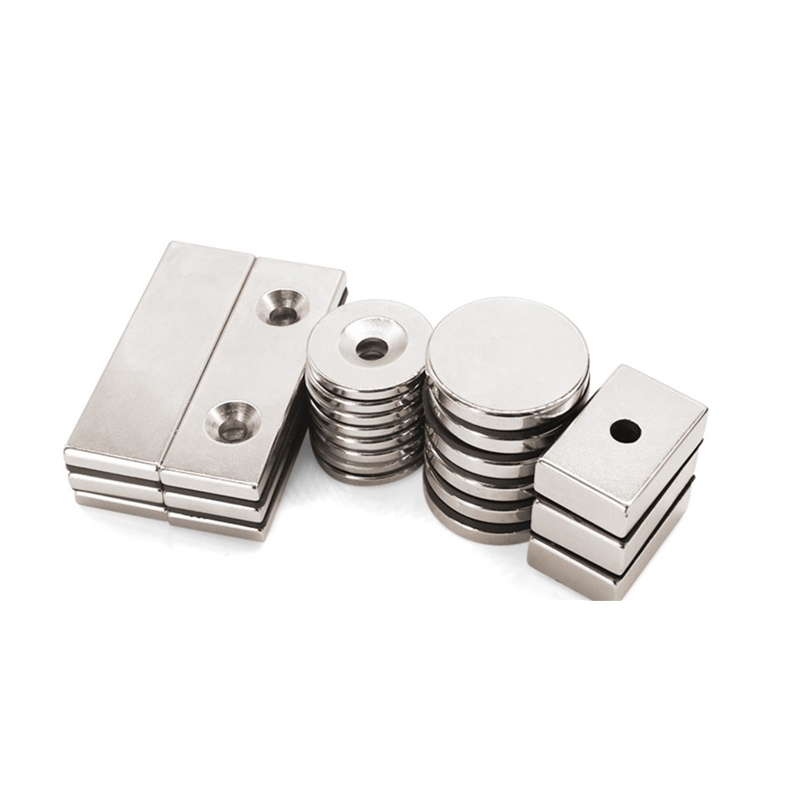
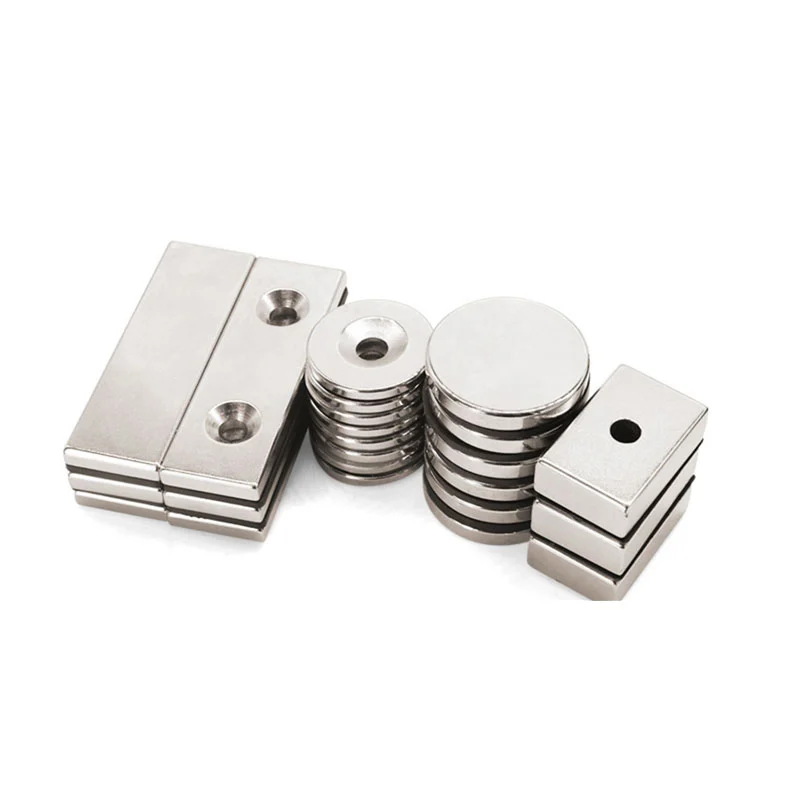
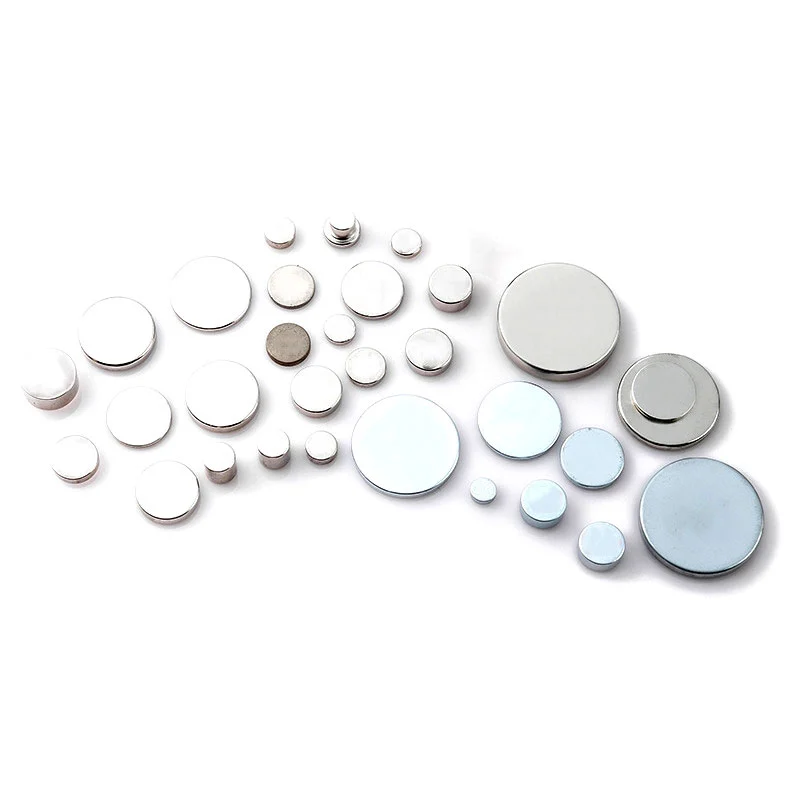
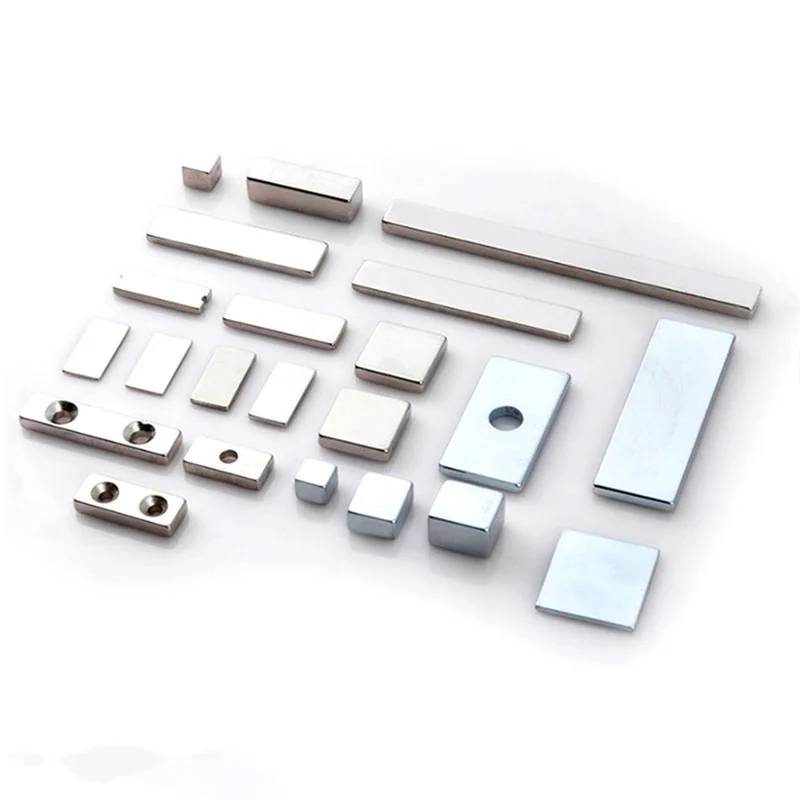
Yes. We produce custom block magnets, ring magnets, arc segments, discs, countersunk magnets with screw holes and special-shaped parts to your CAD files. Tolerances down to ±0.02 mm are achievable on ground surfaces, and we can supply magnetised or unmagnetised, with or without coatings and adhesives.
Do you provide free samples for testing in our equipment?
Yes. We supply free samples of standard sizes for evaluation, and low-cost tooling samples for custom geometries. Each sample shipment includes a technical datasheet with demagnetisation curves across the relevant temperature range, so your engineers can validate performance before mass production.
What certifications and test reports are supplied with each order?
Depending on your requirements we provide material certificates, dimensional inspection reports, magnetic flux and Br/Hcj test data, coating thickness reports, ASTM B117 salt spray results, REACH and RoHS declarations, and MSDS for air and sea freight. Our quality system is certified to IATF 16949:2016 and ISO 9001:2015.
What are your lead times and minimum order quantities for industrial magnet orders?
Standard grades and sizes typically ship within 7–15 working days. Custom tooling and coated parts usually require 20–30 working days. Minimum order quantities are flexible and depend on material and geometry — contact us with your annual volume and we will structure a supply plan that fits your production schedule.
Request Industrial Application Engineering Support
Our engineering team specialises in industrial magnetic solutions and provides comprehensive application support including material selection, thermal performance analysis, magnetic circuit design and integration recommendations. We offer free sample magnets for testing in your actual operating conditions, detailed technical datasheets with performance curves across temperature ranges, and CAD models for seamless integration into your industrial equipment designs.
We use cookies to offer you a better browsing experience, analyze site traffic and personalize content. By using this site, you agree to our use of cookies.
Privacy Policy